In modern-day lab environments, the large capacity refrigerated centrifuge factory is not just a separation apparatus—it is precision engineering. With simple-to-view digital displays and microprocessor controls, it makes it easy for scientists to quickly adjust variables like acceleration and deceleration rates. Other models come equipped with onboard diagnostics that analyze rotor condition and operating performance. High-end safety features like automatic lid interlocks and imbalance detection offer protection at every cycle. With more rapid and consistent processing needed in industries, large capacity refrigerated centrifuge factory technology keeps up with stability, precision, and greater throughput capability.
Clinical laboratory environments utilize large capacity refrigerated centrifuge factory as an important tool for proper diagnosis. Blood banks utilize it to efficiently isolate red cells, plasma, and platelets. Research laboratories employ large capacity refrigerated centrifuge factory to examine tissue samples for cellular and molecular studies. In the energy industry, it assists in the manufacture of biofuels by isolating the biomass components. Food scientists employ large capacity refrigerated centrifuge factory to reclaim fats and purify proteins while preparing products. The numerous applications reflect its capacity to enhance data reliability, process control, and yield output in a wide variety of industries and research applications.
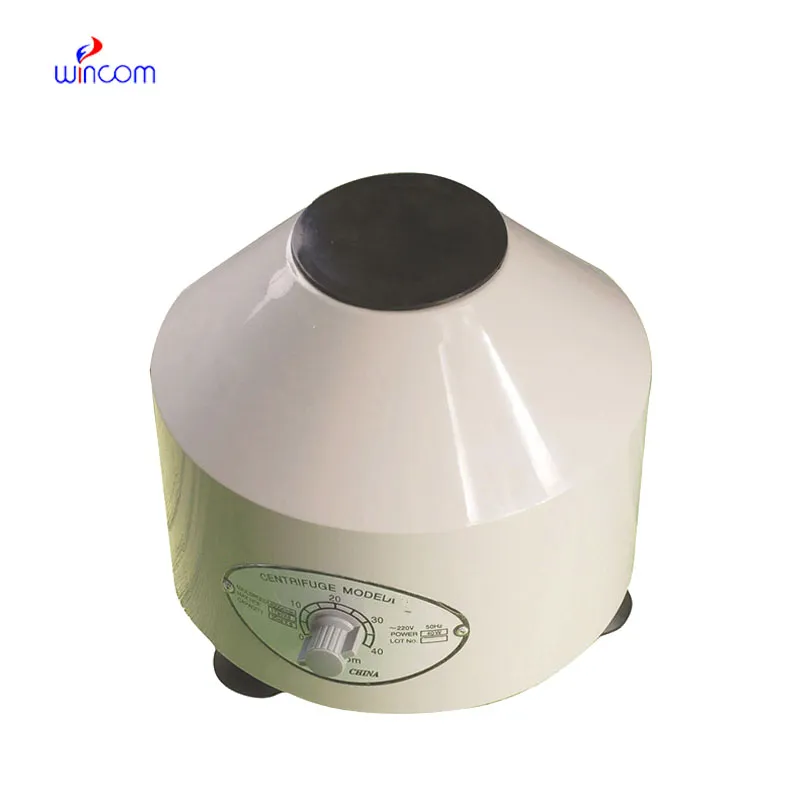
{Keywords} of the future will unprecedentedly advance in performance and design. Future systems will feature adaptive balancing technology that adjusts to dynamic loads in real time. Intelligent rotors will track stress and fatigue in real time, allowing for extended service life. With IoT connectivity, multiple large capacity refrigerated centrifuge factory units will be remotely managed to streamline laboratory networks. In biomedical applications, miniaturized devices will facilitate high-throughput screening with low sample volumes. These advancements are a step toward smarter, faster, and greener devices that revolutionize how separation processes are controlled in modern science.
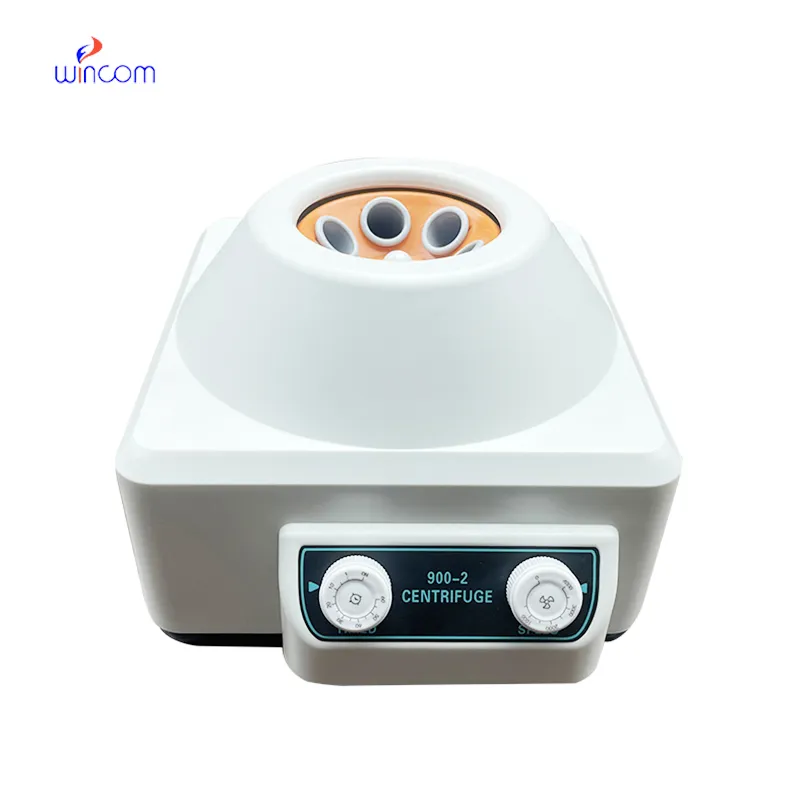
Maintenance of large capacity refrigerated centrifuge factory is essential to lab safety and data integrity. Cleaning should be performed immediately following every operation, with special attention to the elimination of any liquid spills or residues from samples. The rotor should always be handled gently, placed in an upright position during storage, and never subjected to shock. Periodic inspection of lid locks and gaskets ensures airtight operation. Power cord and fuse conditions should also be checked by operators. Annual servicing by skilled technicians adds lifespan. Through regular care processes, large capacity refrigerated centrifuge factory safely and accurately continues to operate.
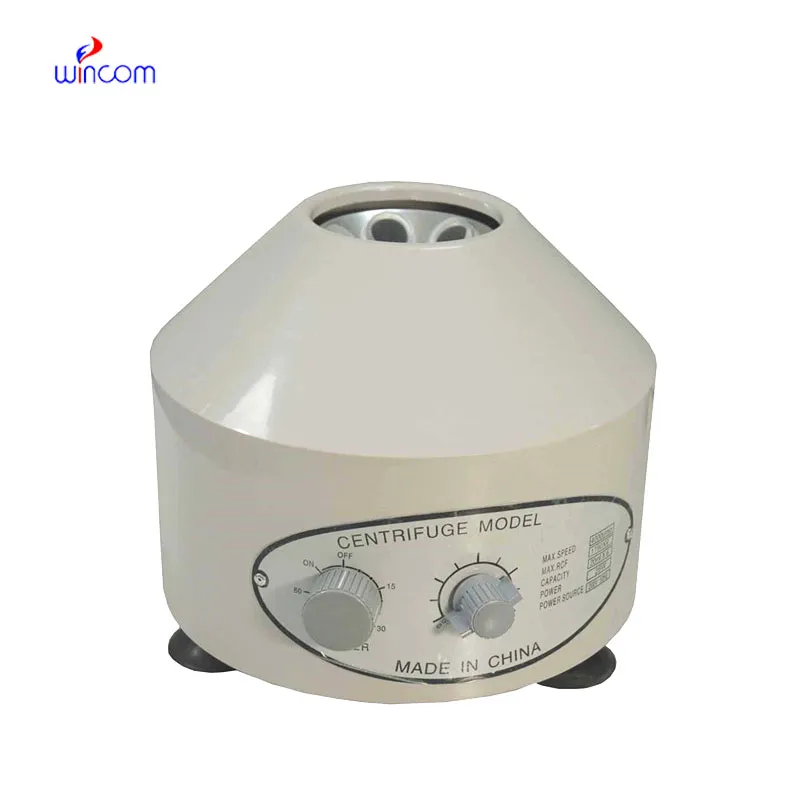
Scientific and industrial applications use the large capacity refrigerated centrifuge factory for its ability to differentiate between mixes with high precision. It relies on the force of centrifugal, which pushes particles off center, leading to density stratification. The method is vital in research, medicine, and engineering. From cell constituents separation to the separation of liquids, large capacity refrigerated centrifuge factory make many analytical and production processes easier. Newer models focus on minimizing vibration, maximizing balance, and the use of smart sensors to monitor data in real time. All these advancements have made large capacity refrigerated centrifuge factory faster, safer, and more efficient than before.
Q: What are the main components of a centrifuge? A: Key components include the rotor, motor, control panel, safety lid, and chamber, each working together to achieve precise separation. Q: How can I verify that a centrifuge is functioning correctly? A: Check that the machine runs smoothly without any unusual vibrations or noises, check the speed accuracy and evaluate the results to ensure consistent separation. Q: Is it safe to open a centrifuge immediately after use? A: No, the device should come to a complete stop before opening to avoid injury or sample disruption. Q: How should a centrifuge be stored when not in use? A:Store it unplugged, covered, and in a dry, dust-free environment to protect internal components from moisture and corrosion. Q: Can centrifuge operation be automated? A: Yes, modern models include programmable controls and digital interfaces that allow automated speed, time, and temperature settings.
The water bath performs consistently and maintains a stable temperature even during long experiments. It’s reliable and easy to operate.
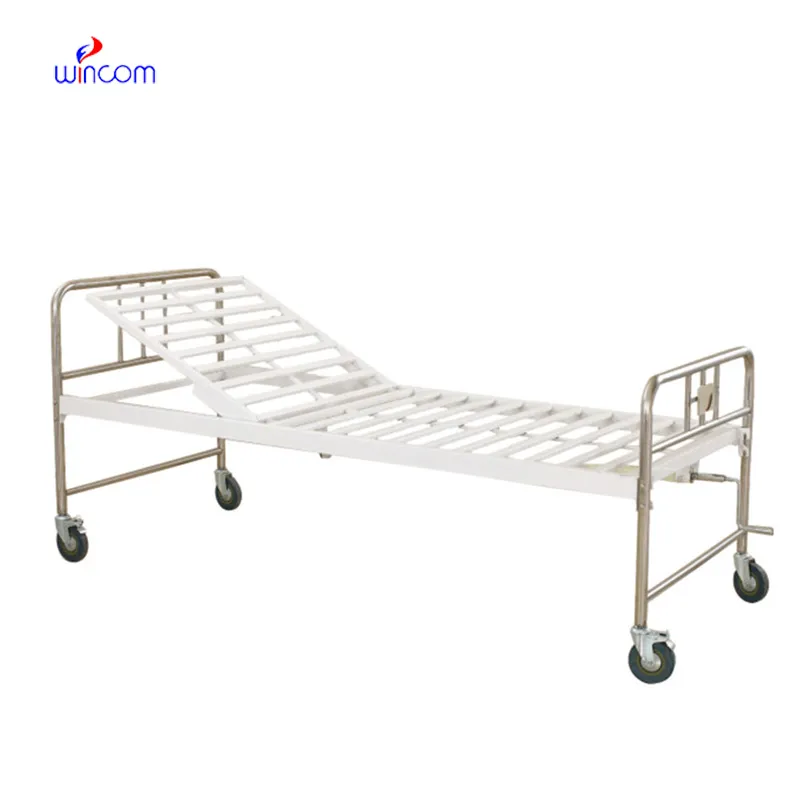
The hospital bed is well-designed and very practical. Patients find it comfortable, and nurses appreciate how simple it is to operate.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We’re looking for a reliable centrifuge for clinical testing. Can you share the technical specific...
Could you share the specifications and price for your hospital bed models? We’re looking for adjus...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China
 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko