Crafted specifically for precision, the refrigerated high speed centrifuge factory is additionally improved by digital and mechanical enhancements. Intelligent balancing systems automatically eliminate unbalanced loads, improving performance as well as safety. Materials such as reinforced polymers and high-grade aluminum are becoming standard in rotor production, reducing wear and maximizing life in operation. Real-time sensors of temperature and speed offer feedback for reliable results. These developments not only improve separation efficiency but also allow for the achievement of stringent laboratory standards. With increasing research needs, refrigerated high speed centrifuge factory technology develops further to ensure better reliability and reproducibility.
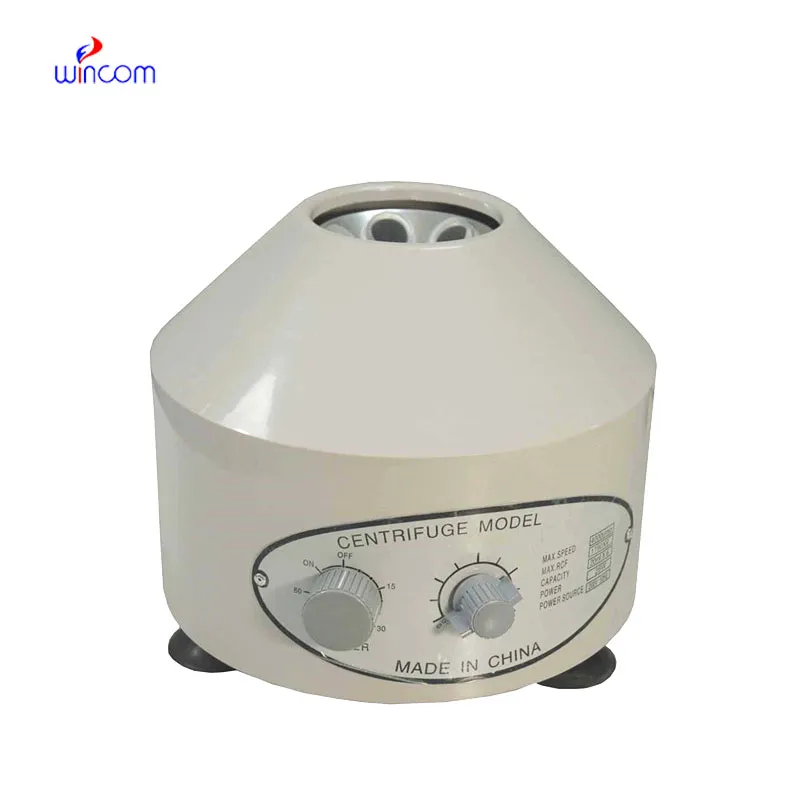
From research in the laboratory to large-scale production, refrigerated high speed centrifuge factory devices have a place in processes requiring precision and efficiency. They purify reaction mixtures and solvents in chemical production. Hospitals rely on refrigerated high speed centrifuge factory for the testing of patients and therapeutic treatment. In farming, refrigerated high speed centrifuge factory are used to study plant biology and develop fertilizer formulations. In brewing and winery operations, they provide consistency within products by filtering out impurities. Even environmental engineers rely on refrigerated high speed centrifuge factory to filter sediment as well as identify contaminants. Such wide-ranging functionality demonstrates its vital position in contemporary technology and applied sciences.
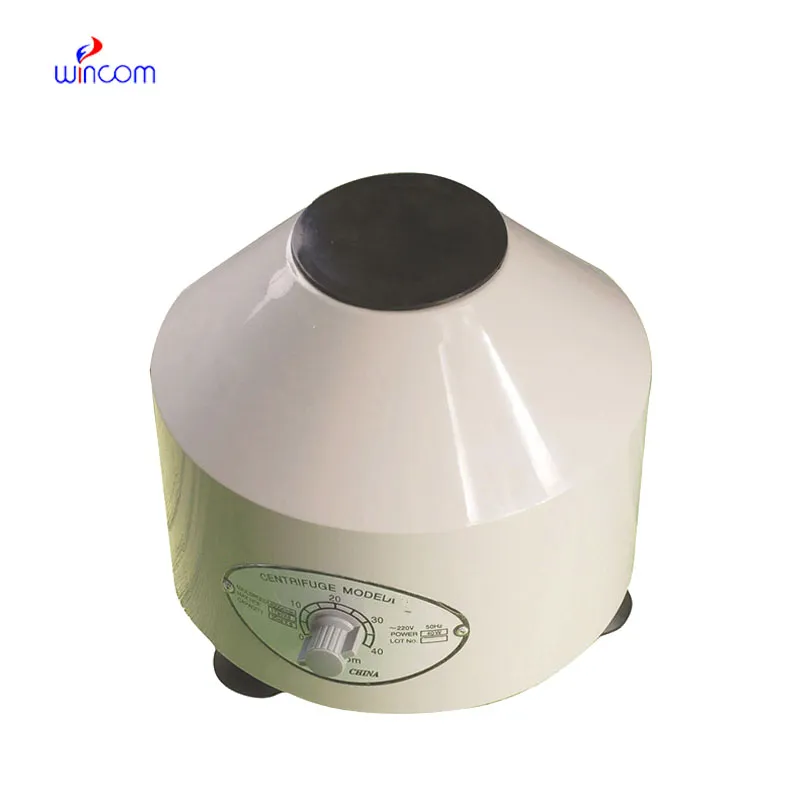
Advances in automation and material science will shape the future of refrigerated high speed centrifuge factory. Composite lightweight materials will offer increased speed and reduced mechanical stress. Integrated AI controls will streamline rotor performance and balance in real time. The addition of remote operation and touchless interfaces will increase accessibility in sterile environments. As data-driven laboratories expand, refrigerated high speed centrifuge factory will be connected to cloud-based systems for predictive diagnostics and performance analytics. All these innovations will create a new generation of smart instruments with the capacity to enable high-throughput, complex applications with precision.
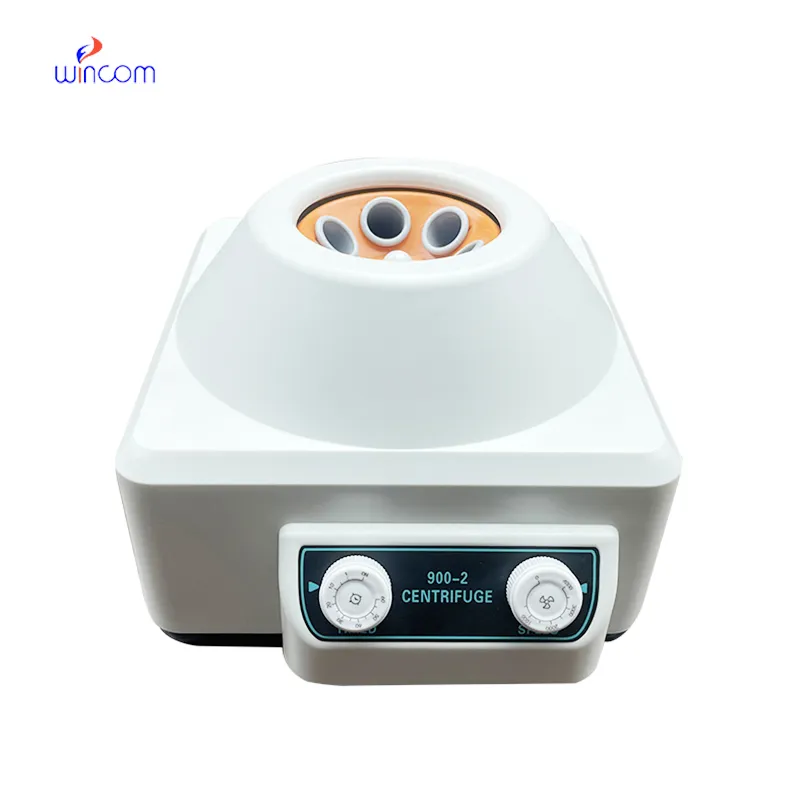
Well-maintained refrigerated high speed centrifuge factory assure trouble-free operation and optimize equipment longevity. Users must ensure balanced loading to prevent excessive stress to bearings. Regular cleaning of the rotor, chamber, and seals reduces cross-contamination. Regular lubrication and calibration ensure mechanical accuracy. Logs of maintenance, checklists, and other records facilitate quality control and inspection for compliance. Internal humidity and dust exposure should be reduced. Laboratories use preventive maintenance instructions to guarantee that refrigerated high speed centrifuge factory delivers constant high performance with little downtime and repair.
Scientific and industrial applications use the refrigerated high speed centrifuge factory for its ability to differentiate between mixes with high precision. It relies on the force of centrifugal, which pushes particles off center, leading to density stratification. The method is vital in research, medicine, and engineering. From cell constituents separation to the separation of liquids, refrigerated high speed centrifuge factory make many analytical and production processes easier. Newer models focus on minimizing vibration, maximizing balance, and the use of smart sensors to monitor data in real time. All these advancements have made refrigerated high speed centrifuge factory faster, safer, and more efficient than before.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
This x-ray machine is reliable and easy to operate. Our technicians appreciate how quickly it processes scans, saving valuable time during busy patient hours.
I’ve used several microscopes before, but this one stands out for its sturdy design and smooth magnification control.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We’re looking for a reliable centrifuge for clinical testing. Can you share the technical specific...
We’re interested in your delivery bed for our maternity department. Please send detailed specifica...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China
 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko